How does PLC control improve machine performance? This question matters wherever a machine must run accurately, safely, and repeatedly. In a production line, small delays can become costly losses. A sensor may detect a jam, a motor may respond too slowly, or an actuator may move beyond its intended position. PLC control connects these events through programmed logic, creating faster and more consistent machine responses.
Dick Morley, widely recognized as the father of the programmable logic controller, described it clearly: “The PLC is a computer designed for the factory floor.” That practical definition still applies today. Unlike scattered relay systems, a PLC can monitor inputs, process conditions, and command outputs within milliseconds. Operators can also review alarms, cycle times, and fault histories from a human-machine interface. These details support better maintenance decisions and more reliable production planning.
This introduction explores seven effective ways PLC control improves machine performance. The discussion covers response speed, process accuracy, downtime reduction, energy management, diagnostics, flexibility, and safety coordination. Each benefit depends on proper programming, suitable sensors, and disciplined maintenance. A PLC alone cannot repair a poorly designed machine. That point is easy to overlook. A poorly tuned control loop may still create vibration, waste, or uneven output. Real improvement comes from testing the system under actual operating conditions, measuring results, and correcting weak assumptions. Even experienced engineers must revisit the logic when materials, workloads, or production targets change.
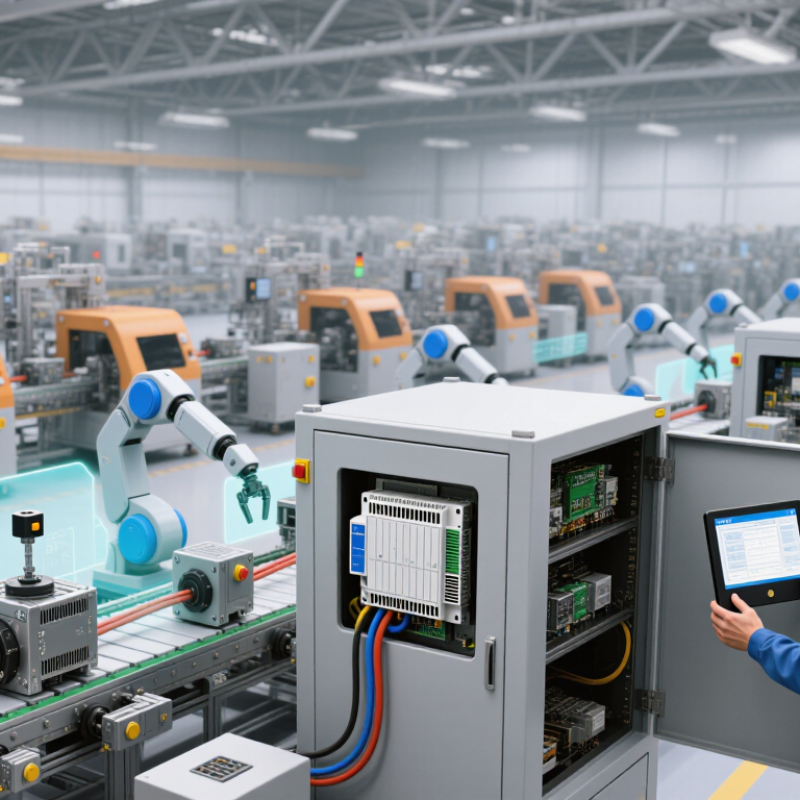
The role of PLCs in modern machine performance extends beyond basic on-and-off control. A PLC reads sensors, processes logic, and adjusts actuators within milliseconds. This creates seven practical advantages: faster sequencing, steadier motion, accurate counting, safer interlocks, lower energy use, predictive alarms, and easier troubleshooting. Operators can see a jam developing before a conveyor stops. That small warning matters.
A well-designed PLC also connects machine data with production systems. It records cycle times, rejects, temperature changes, and motor loads. Engineers can compare yesterday’s output with today’s performance. The World Economic Forum’s Global Lighthouse Network reports productivity improvements of up to 50% in advanced manufacturing sites using connected technologies. A PLC cannot create that result alone. However, it supplies dependable control data for better decisions.
Energy control deserves close attention. The U.S. Department of Energy reports that motor-driven systems consume about 23% of total U.S. electricity. PLC logic can stop idle motors, coordinate startup sequences, and detect abnormal loads. These actions reduce waste without changing the entire machine. Yet a PLC is not magic. Poor sensor placement, unclear alarm messages, or rushed programming can create new downtime. During commissioning, technicians should test every failure condition, not only the normal cycle. That discipline is often missed.
A programmable logic controller (PLC) improves machine performance by making control decisions at predictable intervals. This timing reduces variation between cycles, especially when conveyors, valves, and actuators must respond together. With calibrated sensors, the PLC can compare target values with actual readings and correct small deviations quickly. The result is steadier pressure, temperature, speed, and positioning. More precise control usually means fewer rejects and more consistent products. Small differences matter.
A PLC also stores approved operating recipes, so operators can repeat settings across shifts without relying on memory. Interlocks prevent conflicting commands, while alarms identify issues such as low pressure or delayed motion. Built-in diagnostics shorten troubleshooting by showing which input or output changed first. Motion sequences can be synchronized, reducing unnecessary pauses and mechanical shock. Production data can reveal drift before it becomes a visible defect. These functions support safer, more repeatable work.
In practice, performance depends on more than the PLC. Dirty sensors, loose wiring, and poor tuning can still create unstable results. A fast scan cannot repair inaccurate measurements. Engineers should test each control loop under real load, review alarm limits, and compare samples from different shifts. Initial settings may look correct but fail after temperature or material changes. That weakness deserves attention. Regular calibration, documented changes, and operator feedback keep precision meaningful rather than merely theoretical.
A PLC improves machine performance by turning routine signals into useful evidence. During a plant trial, technicians can watch motor current, cycle time, temperature, and sensor status from one diagnostic screen. A rising temperature may appear before a conveyor stops. An intermittent input may reveal a loose cable, not a failed motor. These details shorten troubleshooting, especially when alarms include timestamps and first-out logic. Clear diagnostics matter.
A PLC supports this approach by comparing live values with operating limits and recording abnormal patterns. The 2023 Smart Manufacturing and Operations Survey found that 86% of manufacturers viewed smart technologies as important to future competitiveness. Monitoring is no longer optional for many plants.
Yet, a PLC is not a crystal ball. Poorly set alarm limits can create noise, while missing sensor calibration can produce false confidence. ISA-18.2 guidance recommends managing alarms throughout their life cycle, including review and rationalization.
In practice, a useful screen shows the failed input, recent values, and safe recovery steps. Keep it simple. A technician standing beside a noisy machine needs answers, not decorative graphics.
Some teams still log faults manually, which weakens the data trail and delays learning. That gap deserves honest review.
A programmable logic controller can turn scattered machine actions into one measured workflow. It starts motors, checks sensors, controls timing, and stops unsafe sequences in milliseconds. This consistency reduces waiting between operations and limits avoidable operator errors. A PLC also records cycle times, alarms, and stoppages. Managers can then find the slow station instead of guessing. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of leaders expect smart manufacturing to improve competitiveness within three years. That expectation reflects a practical shift toward data-led production.
The productivity gains become clearer on the factory floor. A controlled filling line can maintain valve timing within a narrow range. A packaging cell can reject damaged units before they reach final inspection. Predictive signals can also expose rising temperature or vibration before a breakdown. Rockwell Automation’s 2024 State of Smart Manufacturing Report found that 95% of manufacturers are investing in, or planning to invest in, artificial intelligence and machine learning within five years. PLC data provides the dependable operational layer those tools require. Still, automation is not magic. Poor sensor placement or unclear logic can make a fast machine fail faster.
Tips: Map the process before programming. Measure baseline cycle time, downtime, scrap, and energy use. Use clear alarm messages, not confusing codes. Review PLC data weekly with operators. Their experience often reveals problems dashboards miss. Leave room for improvement.
A programmable logic controller can make machine safety visible and repeatable. During commissioning, engineers can connect guard switches, light curtains, emergency stops, and pressure sensors to defined control logic. The system can then stop motion before a hand reaches a danger zone. The Occupational Safety and Health Administration estimates that machine guarding failures cause about 18,000 amputations and 36,000 serious injuries annually in the United States. These figures make safety logic more than a technical feature.
Seven practical improvements stand out: monitored interlocks, controlled stopping, fault diagnostics, alarm history, modular inputs, recipe management, and condition monitoring.
A PLC can reject an unsafe sequence instead of relying on operator memory. It can also display a clear fault, such as “low clamp pressure,” instead of a vague stop signal. NIST Special Publication 800-82 Revision 3 identifies availability, safety, and controlled access as essential priorities for operational technology. Therefore, separating control permissions and recording changes can reduce avoidable risk.
Adaptability matters when products, tools, or production speeds change. Engineers can adjust recipes, timing windows, and sensor thresholds without rebuilding the entire control cabinet. Modular programming also supports new stations and inspection devices.
Still, a PLC is not a magic shield. Poorly written logic can hide hazards, and excessive alarms can train operators to ignore warnings. The National Safety Council’s Injury Facts 2024 estimated U.S. work-injury costs at 167 billion dollars for 2022, so every safety function deserves testing, documentation, and honest review.
PLC control improves machine performance by turning scattered signals into usable maintenance information. It monitors cycle times, motor loads, temperatures, and sensor responses continuously. This visibility helps technicians find abnormal behavior before a small fault becomes a stopped production line. Alarm histories also show repeated problems, such as a conveyor sensor failing every Friday afternoon.
Maintenance becomes simpler when the PLC records clear fault codes and operating conditions. A technician can see which input changed, when it changed, and what action followed. Guided checks reduce guesswork and shorten troubleshooting time. The controller can also schedule lubrication reminders, inspection intervals, and component replacement based on actual machine hours. Small details matter. Poor tag names or missing comments still create confusion.
Performance management improves through consistent settings and measurable data. Operators can monitor output, downtime, rejected parts, and recovery time from one interface. Managers can compare shifts without relying only on handwritten notes. A PLC can stabilize speed, timing, and process limits, reducing variations between operators. However, data is not automatically useful. An overloaded dashboard may hide the important warning. Regular reviews are needed to remove false alarms, verify sensors, and adjust thresholds. Reliable control comes from disciplined maintenance, accurate documentation, and technicians who question the data.
| No. | PLC Improvement Method | Machine Performance Area | Key Data Dimension | Illustrative Reference Value | Maintenance Benefit | Recommended KPI |
|---|---|---|---|---|---|---|
| 1 | Automated Sequence Control | Consistent machine cycles and repeatable operations | Cycle-time variation | Target variation: within ±2% of the standard cycle time | Reduces operator-dependent errors and simplifies fault tracing by sequence step | Average cycle time; cycle-time deviation |
| 2 | Real-Time Monitoring | Visibility of speed, temperature, pressure, position, and status | Data sampling and alarm response | Typical PLC scan times: milliseconds; alarm response should be defined by the process risk assessment | Makes abnormal trends visible before they become production stoppages | Alarm response time; abnormal-condition count |
| 3 | Interlock and Safety Logic | Prevention of unsafe or incorrect operating conditions | Fault prevention and safe-state activation | 100% verification of defined permissives, interlocks, and emergency-stop circuits during commissioning | Provides clear diagnostic states instead of relying on manual inspection | Safety-trip count; interlock fault rate |
| 4 | Condition-Based Maintenance | Early detection of wear, overheating, leakage, and drift | Sensor trend limits and rate of change | Use warning and shutdown thresholds based on equipment specifications and historical operating data | Supports planned intervention and reduces unnecessary calendar-based servicing | MTBF; planned-maintenance ratio; warning events |
| 5 | Automatic Fault Diagnostics | Faster identification of electrical, mechanical, and process faults | Fault code accuracy and troubleshooting duration | Record fault timestamp, active condition, first-out signal, and reset history for every stop | Reduces time spent checking unrelated components and improves root-cause analysis | MTTR; repeat-fault percentage |
| 6 | Recipe and Parameter Management | Fast, controlled changeover between products or operating modes | Changeover time and parameter accuracy | Store approved setpoints with user permissions, revision history, and validation checks | Prevents manual setting errors and makes repeat production easier to reproduce | Changeover duration; setup-related defects |
| 7 | Production Data and OEE Reporting | Continuous improvement based on actual operating data | Availability, performance, and quality | OEE = Availability × Performance × Quality; calculate from production counts and downtime records | Creates a traceable record for downtime analysis, capacity planning, and maintenance priorities | OEE; downtime minutes; first-pass yield |
Note: Reference values are general engineering guidelines. Actual targets should be established from machine specifications, risk assessments, historical operating data, and validated production requirements.
A PLC reads sensors, processes logic, and controls actuators within milliseconds. It coordinates motors, valves, conveyors, and safety interlocks. Small warning signals matter.
It makes control decisions at predictable intervals. Calibrated sensors help maintain stable pressure, temperature, speed, and positioning. Small differences can still appear.
Yes, diagnostic data can show which input or output changed first. Operators may detect a jam before the conveyor stops. The result is not guaranteed.
It can stop idle motors, coordinate startup sequences, and detect abnormal loads. These actions reduce waste without replacing the entire machine. Every saving counts.
It can record cycle times, rejects, alarms, temperature changes, motor loads, and stoppages. Engineers can compare yesterday’s output with today’s results. Data needs context.
A PLC turns separate machine actions into one measured workflow. It reduces waiting, limits repeated operator errors, and identifies slow stations. Fast control helps.
Dirty sensors, loose wiring, poor tuning, and unclear alarms can cause unstable results. A fast scan cannot repair inaccurate measurements. This weakness is often missed.
They should test normal cycles and every realistic failure condition. Tests should include low pressure, delayed motion, sensor loss, and abnormal motor loads. Shortcuts create doubt.
How does PLC control improve machine performance? By coordinating sensors, actuators, and programmed logic in real time, a PLC enables machines to respond accurately and consistently to changing operating conditions. This improves control precision, reduces process variation, and supports more consistent product quality. Automated sequences also minimize manual intervention, shorten cycle times, and increase overall productivity.
PLC systems can continuously monitor machine status, identify abnormal conditions, and provide useful diagnostic information before minor issues become serious failures. This helps reduce downtime and allows maintenance teams to locate problems more efficiently. Integrated safety logic can support safer operation, while flexible programming makes it easier to adapt equipment to new products, process requirements, or production volumes. In addition, performance data and operating records help teams evaluate efficiency, plan preventive maintenance, and improve long-term machine management. Overall, PLC control creates a more reliable, adaptable, and manageable production environment.
Jinli Machinery